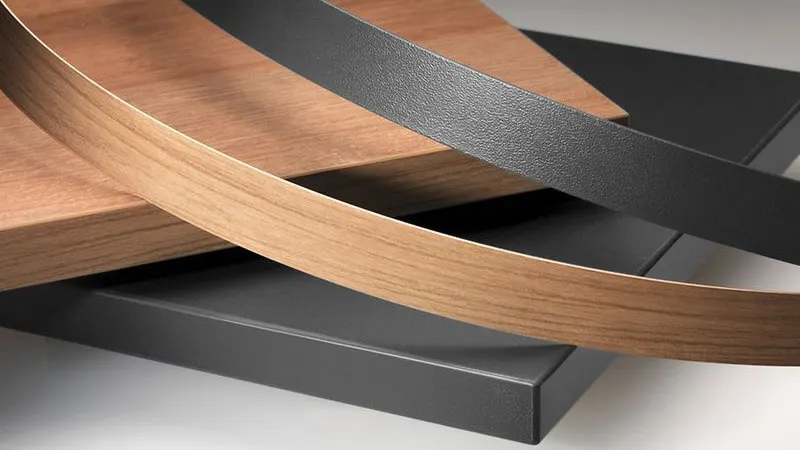
The edge band is the first impression of furniture quality; customers often judge a piece by its edges. Here are the mistakes we see most often in the field, with solutions.
1. Cold panels
In winter, panels going straight from the warehouse to the line freeze the adhesive before it wets the surface. Fix: Condition panels to at least 18 °C and use panel preheating where possible.
2. Wrong adhesive temperature
Too low means poor wetting; too high causes charring and stringing. Fix: Work within the data-sheet range and measure tank and roller temperatures separately.
3. Too much adhesive
Excess adhesive gives thick, visible glue lines and squeeze-out. Fix: Set coat weight by panel thickness and density; PUR usually needs less.
4. Insufficient pressure
Without enough pressure the band doesn't make full contact within the open time. Fix: Check pressure roller settings and wear regularly.
5. Wrong open time
An adhesive that doesn't suit the line speed skins over before the band touches. Fix: Choose an open time that matches your feed speed.
6. Missing primer on the band
ABS and PP bands without primer bond poorly. Fix: Order primed bands or use a suitable primer.
7. Dirty tank and charred adhesive
Adhesive held hot for too long chars and particles block the nozzle. Fix: Lower tank temperature during breaks, clean regularly and consider low-char PO grades.
8. Incorrect PUR cleaning
PUR left to cure in the tank seriously damages the machine. Fix: Use a PUR flushing agent at stoppages and follow the manufacturer's procedure.
Quick checklist
- Panel temperature ≥ 18 °C
- Adhesive temperature within data-sheet range
- Coat weight set to panel type
- Pressure rollers clean and adjusted
- Band suitably primed
- Tank clean, adhesive not charred
If problems persist, we can visit your line for an on-site analysis.